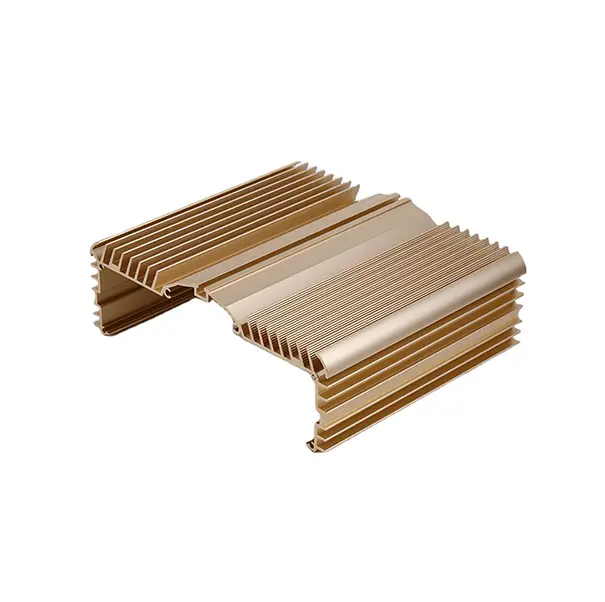
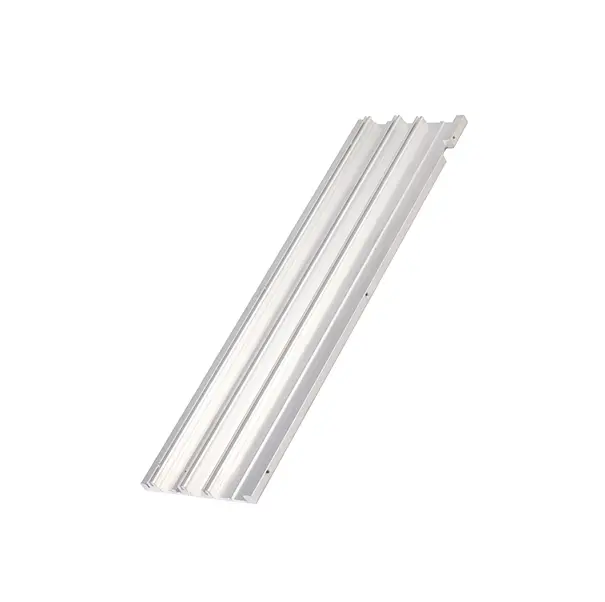
Custom Aluminum 6061 6063 Heatsink
Extruded heatsinks in the two grades named across the range.
Home › Aluminum Extrusion — Custom Profiles & Parts
Custom aluminum extrusion in 6061 and 6063: heatsinks, enclosures, pipes and profiles produced to your design — and finished by the machining and coating lines in the same factory.
| Grades | Aluminum 6061, 6063 (named in the heatsink product) |
|---|---|
| Evidenced products | Custom Aluminum 6061 6063 Heatsink; Custom Extruded Enclosure; Custom Aluminum Extruded Pipe; Extrusion for Doors and Windows; Extrusion According To Your Design |
| Finishes | Anodizing (evidenced: anodized heatsink product) |
| Secondary work | Cutting, CNC machining, drilling in-house |
| Order policy | No fixed MOQ; small-batch trial production supported |
Extruded heatsinks in the two grades named across the range.
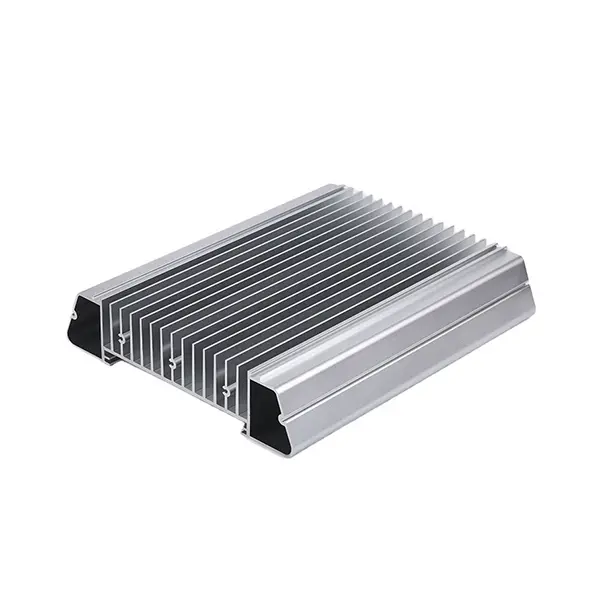
Heatsinks supplied anodized for corrosion protection and finish.
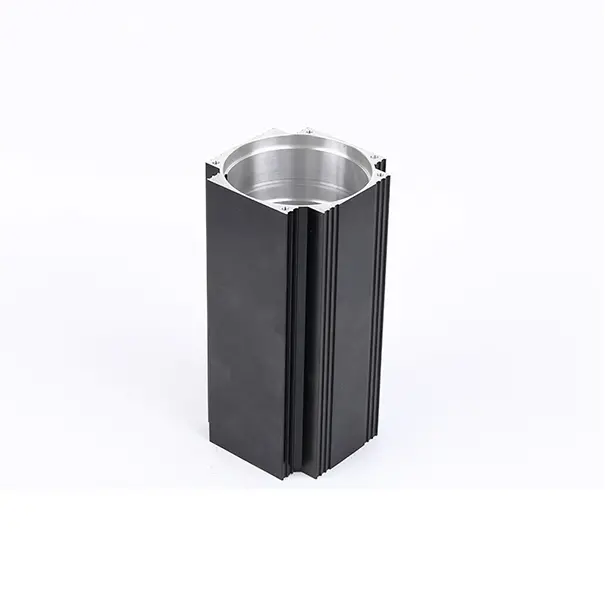
Extruded aluminum enclosures for electronics and equipment.
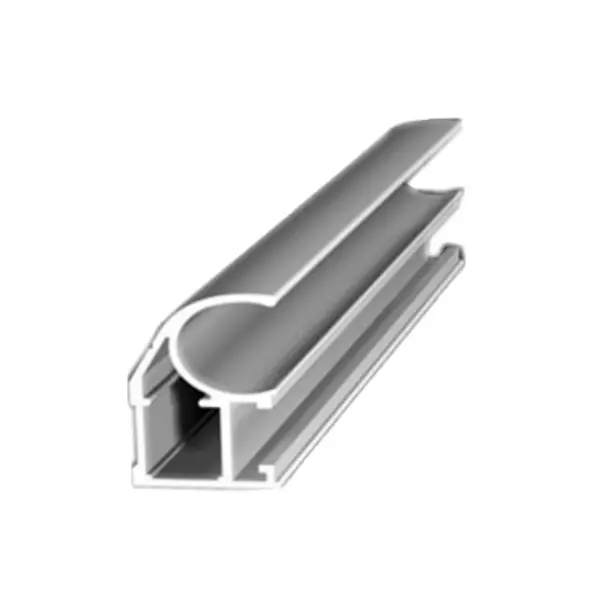
Extruded aluminum pipe and tube profiles to design.
Door and window profiles from the architectural end of the range.
Fully custom profiles developed from your section drawing.
The range's most telling product name is its most literal: Custom Aluminum Extrusion According To Your Design. Extrusion is the process of pushing heated aluminum through a shaped die to produce a constant cross-section profile — and the profile is whatever the die says it is. A custom extrusion programme therefore starts with your section drawing: the profile you designed, extruded in 6061 or 6063, cut to length and finished.
Around that core, the range covers the classic extrusion families: heatsinks (plain and anodized), enclosures, pipes, and door & window profiles. Each family is a named product, which means the dies, handling and finishing routes for those profiles are production routine here.
An extrusion is rarely the finished part. It needs cutting to length, holes, slots, end machining, and often an anodized finish — the range's anodized heatsink product shows that route in one name. All of those steps live in this factory: CNC machining for the features, anodizing for the finish, CMM inspection for the critical dimensions. The profile supplier who only extrudes hands you a semi-finished product and a second sourcing problem; this route hands you parts.
The same integration lets the review compare honestly across processes. A housing with a constant section belongs to extrusion; one with varying geometry belongs to casting or machining. The quote will say which — with prices for the route recommended.
Send the section drawing (or the finished-part drawing and let us derive the section), the grade — 6061 or 6063 per this range — lengths, finish and quantities. Profile dies are comparatively economical tooling, and with no fixed MOQ the route from section approval to trial lengths is short. If the part also needs cast or stamped companions, one review can cover the set.
Extrusion programmes stay healthy on two habits. First, treat the section as a contract: once the profile die is proven, changes to the section are tooling events, so the time to argue about a fin, a wall or a channel is at section review, with the die designer in the conversation. Second, plan lengths and downstream machining as one schedule — cut lengths, hole patterns and anodizing batches interact, and programmes that schedule them together waste less metal and less time than programmes that order each step in isolation.
Buyers transferring an existing profile should say so at enquiry. A profile with an existing die, a profile needing a new die, and a profile being re-specified from a sample length are three different projects with three different first steps, and the review will name which one you have before quoting anything.
Tell us the material grade, quantity and finish you need for your custom aluminum extrusions. Our engineers review every drawing for die casting, machining or stamping feasibility before quoting — no obligation.
Send Drawings for a DFM Review